Rocker Clamps
The Next Generation of Fixture Clamping
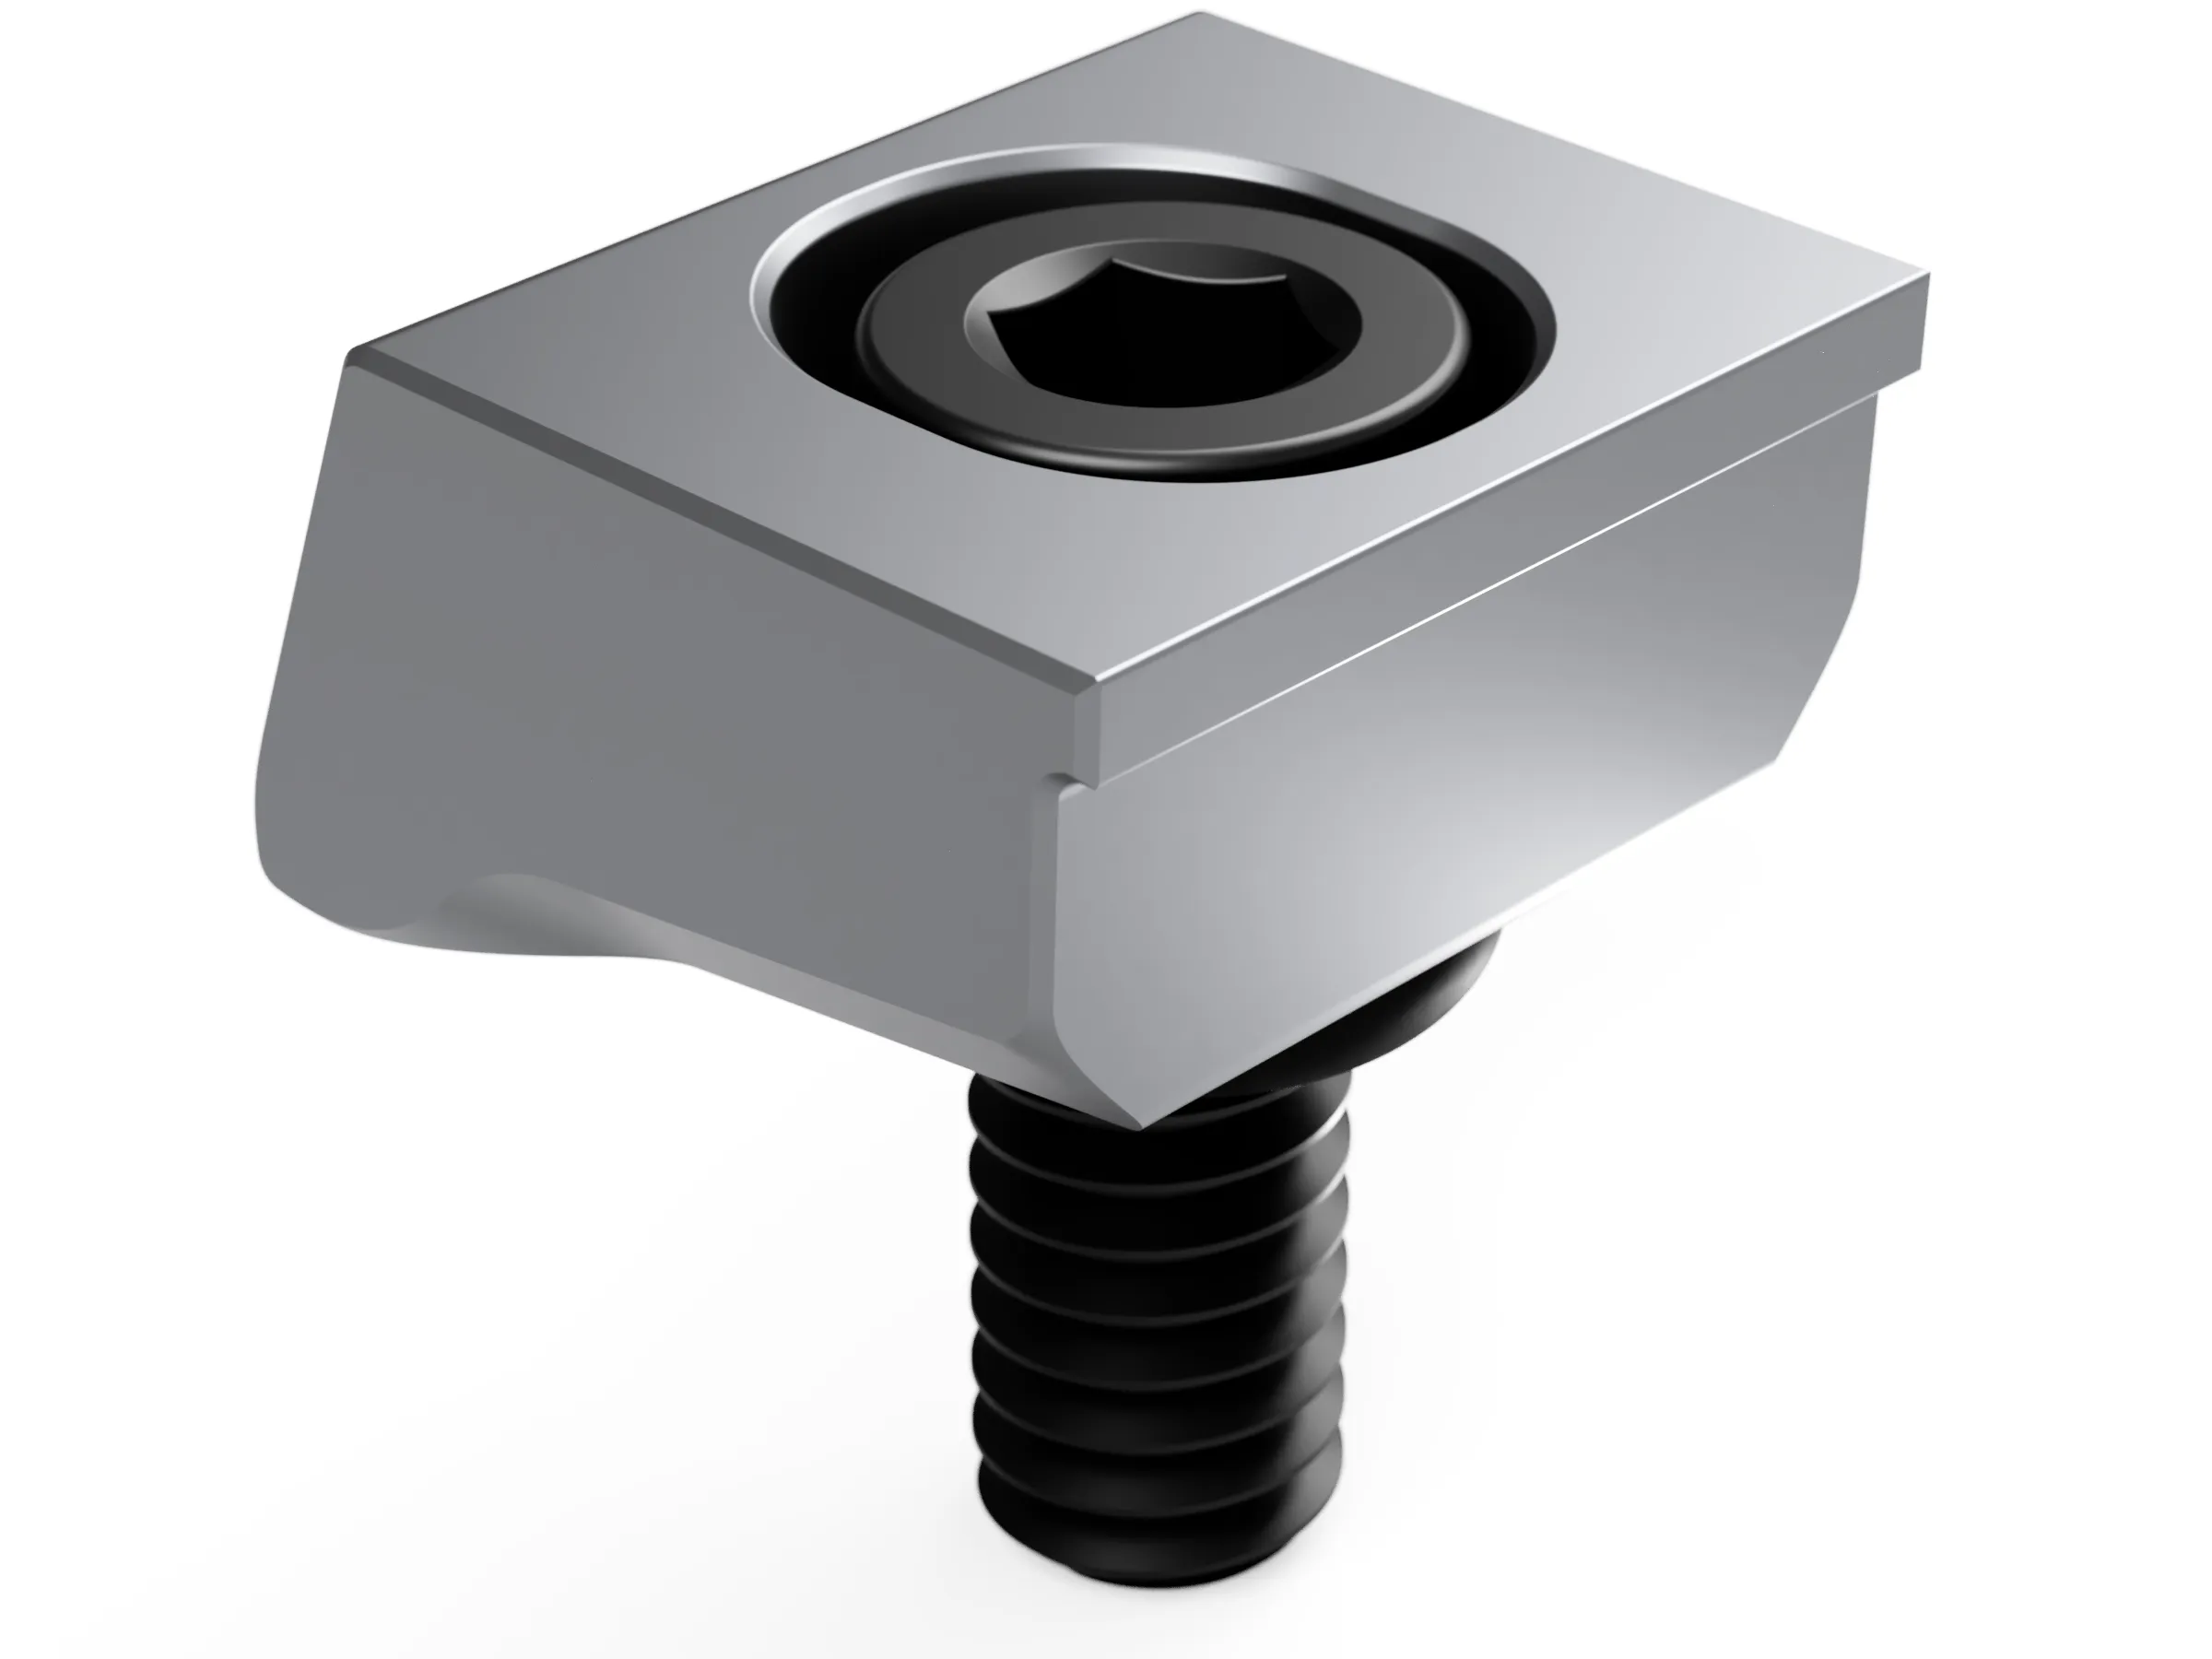
These shop-proven Rocker Clamps are unmatched when it comes to high clamping force in small areas. Each clamp is fully CNC machined for true-to-model geometry and rocks on compound pivot surfaces for higher clamping force and reduced pocket wear. When properly engaged, it sits parallel to the top of the fixture, so a glance down the row confirms every part is clamped. Choose Flat, Serrated or Brass faces, each sold as a single clamp or a 10 pack.
- Precision, True-to-Model Geometry
- Compound Radii Contact Surfaces
- Flat Top Confirms Proper Clamping
- Higher Clamping Force, Less Pocket Wear
- Flat, Serrated & Brass Faces
- Sold as Singles or 10 Packs
- Heavy Chamfered lower edges eliminate chip packing
- 3/4″ and 1″ wide versions
- clamp widths
- 3/4″ & 1″
- clamp widths
- clamp throw
- .035″ & .060″
- clamp throw
- lbs clamping force
- 3,750–6,500
- lbs clamping force
- face types, each in 1 or 10 packs
- 3
- face types, each in 1 or 10 packs
Three Faces for Every Job
Rocker Clamps come in 3/4″ and 1″ widths. Within a width, every face shares the same body, pocket and screw, so you can mix faces on one fixture. Each type is sold as a single clamp or a 10 pack.
1 / 4
Flat Face
A great choice for all-around general use. Use in both OP1 and OP2 work in all materials, including hard metals (>HRC30).
- 3,750 lbs clamping force
- General clamping for 1st or 2nd operations
- All materials, including hard metals (>HRC30)
- Made from hardened tool steel for maximum life
- Max torque: 10 ft-lbs into aluminum, 15 ft-lbs into steel or screw thread inserts
Buy 3/4″ 1 Pack: Flat FaceRC750F-1Buy 3/4″ 10 Pack: Flat FaceRC750F-101″ 1 Pack: Coming soon1″ 10 Pack: Coming soon1 / 4
Serrated Face
The right choice for 1st operation workholding in brass, aluminum, and plastics. Not recommended for materials >HRC30; choose Flat Face instead.
- 3,750 lbs clamping force
- 1st operation workholding
- Brass, aluminum and plastics
- Made from hardened tool steel for maximum life
- Max torque: 10 ft-lbs into aluminum, 15 ft-lbs into steel or screw thread inserts
Buy 3/4″ 1 Pack: Serrated FaceRC750S-1Buy 3/4″ 10 Pack: Serrated FaceRC750S-101″ 1 Pack: Coming soon1″ 10 Pack: Coming soon1 / 4
Brass Face
A great choice for 2nd operation work to reduce cosmetic clamping marks.
- 1,050 lbs clamping force
- 2nd operation work on finished surfaces
- Reduces cosmetic clamping marks
- Made from Rockwell B78 hardness 360 Brass
- Max torque: 6 ft-lbs; low profile 1/4-20 socket head cap screw, 1/8″ hex drive
Buy 3/4″ 1 Pack: Brass FaceRC750B-1Buy 3/4″ 10 Pack: Brass FaceRC750B-101″ 1 Pack: Coming soon1″ 10 Pack: Coming soon
Why Pierson Rocker Clamps
- Extremely accurate geometry. Fully CNC machined for true-to-model geometry, so the clamp in your fixture matches the clamp in your CAD model. Cut the pocket to the drawing and every clamp fits the same: headache-free fixturing.
- Compound radii contact surfaces. Compound pivot geometry for higher clamping forces and reduced pocket wear.
- Flat top for visual confirmation. The top of the Rocker sits parallel with the fixture top when properly engaged. One look down a row of clamps confirms every part is clamped before you press cycle start.
- Chips clear out. Heavy chamfered lower edges eliminate chip packing, and bottom funnel gullets greatly aid chip evacuation.
- Built to last. Steel Rockers are hardened tool steel for maximum life; Brass Rockers are Rockwell B78 hardness 360 Brass.
- Small footprint. A .750″ x 1.000″ pocket (3/4″ clamp) and a single screw put high clamping force in small areas, so more parts fit on every fixture.
Fixture Design
Pocket Detail
Rocker Clamps drop into a simple milled pocket next to the part and tighten with a single 1/4-20 socket head cap screw. Cut the pocket to this drawing and every clamp fits the same.
- 3/4″ clamp: pocket .750″ x 1.000″ with R.130 corners, cut to a minimum of .125″ deep
- 1/4-20 UNC tapped .550″ deep from the pocket floor (hole location per the drawing)
- .09″–.3″ total clamping height range, depending on pocket depth
- Clamp throw: .035″ (0.9 mm)
- Use with threaded inserts/Helicoils for fixture longevity
- Torque: 10–15 ft-lbs steel Rockers, 5–7 ft-lbs brass Rockers
Top of Rocker will be parallel with fixture top when properly engaged.
Pocket Detail
Rocker Clamps drop into a simple milled pocket next to the part and tighten with a single 3/8-16 socket head cap screw. Cut the pocket to this drawing and every clamp fits the same.
- 1″ clamp: Pocket 1.000″ x 1.300″ with R.130 corners, cut to a minimum of .150″ deep
- 3/8-16 UNC tapped .625″ deep from the pocket floor
- .18″–.55″ total clamping height range, depending on pocket depth
- Clamp throw: .060″ (1.5 mm)
- Use with threaded inserts/Helicoils for fixture longevity
- Torque: steel Rockers 35 ft-lbs into aluminum, 55 ft-lbs into steel or with a threaded insert; brass Rockers 20–25 ft-lbs
Top of Rocker will be parallel with fixture top when properly engaged.
Rocker Clamps Applications
High-Density Fixture Plates
Rows of 3/4″ and 1″ Rocker Clamps hold many parts on one fixture or pallet, and the small pockets leave room for more parts per cycle.
1st Operations in Soft Materials
Serrated Face Rocker Clamps are the right choice for 1st operation workholding in brass, aluminum and plastics.
2nd Operations on Finished Parts
Brass Face Rocker Clamps reduce cosmetic clamping marks when holding finished surfaces in 2nd operation work.
FAQs
1.Which Rocker Clamp face should I choose?
Flat Face is the all-around choice for 1st or 2nd operation work in all materials, including hard metals (>HRC30).
Serrated Face is the right choice for 1st operation workholding in brass, aluminum and plastics. Not recommended for materials >HRC30.
Brass Face is for 2nd operation work, to reduce cosmetic clamping marks.
2.Can I buy a single clamp, or do I need a 10 pack?
Both. Every face type is sold as a 1 pack or a 10 pack, so you can try one, replace one, or outfit a whole fixture.
3.How many clamps do I need?
Every application is different, but the general starting point is to multiply the clamp width times 4. This means a 3/4″ clamp is needed every 3″, and a 1″ clamp every 4″. For light machining, this clamp spacing can be extended but at a minimum, always place clamps at the ends of the part.
4.How do I know a Rocker Clamp is properly engaged?
The top of the Rocker will be parallel with the fixture top when properly engaged. If a clamp's top is tilted, check that clamp before running the job.
5.How tight should I torque Rocker Clamps?
3/4″ clamps: steel Rockers (Flat and Serrated Face) max 10 ft-lbs into aluminum, 15 ft-lbs into steel or screw thread inserts. Brass Rockers max 6 ft-lbs.
1″ clamps: steel Rockers 35 ft-lbs into aluminum, 55 ft-lbs into steel or with a threaded insert. Brass Rockers 20–25 ft-lbs.
6.What screw do Rocker Clamps use?
3/4″ clamps: a 1/4-20 socket head cap screw. Brass Face Rockers use a low profile 1/4-20 socket head cap screw with a 1/8″ hex drive.
1″ clamps: a 3/8-16 socket head cap screw.
7.How do I cut the pocket?
3/4″ clamps: mill a .750″ x 1.000″ pocket with R.130 corners at least .125″ deep, and tap 1/4-20 UNC .550″ deep from the pocket floor.
1″ clamps: mill a 1.000″ x 1.300″ pocket with R.130 corners at least .150″ deep, and tap 3/8-16 UNC .625″ deep from the pocket floor.
See the pocket detail for the hole location. We recommend threaded inserts or Helicoils for fixture longevity.
Downloads
Rocker Clamps
The Next Generation of Fixture Clamping